Engineered load handling, fall-arrest mechanisms, and high-performance safety headgear certified for cross-market compliance.
Strategic shift towards modern aesthetics, executive identification, and thermally stabilized composite polymers across heavy industry.
Black safety helmets have transcended the traditional color spectrum, transitioning from specialized applications to preferred gear for site executives, inspectors, architectural engineers, and high-tech installation personnel seeking professional identity.
Early dark helmets faced challenges with solar heat absorption and degradation. Modern black safety helmets use specialty carbon black masterbatches formulated with UV absorbers and thermal reflective additives to mitigate shell overheating.
Global mega-projects require standardized PPE packages. Buying black safety helmets in bulk directly from certified factories ensures brand uniform aesthetics while satisfying the strict compliance demands of multi-national joint ventures.
Procuring industrial head protection requires understanding impact mechanics, polymer thermodynamics, and regulatory compliance. When industrial procurement specialists buy black safety helmets, they must address common concerns regarding solar radiation absorption, electrostatic dissipation, and structural longevity under severe mechanical strain.
The protective capability of a safety helmet depends on its shell material. For black safety helmets, selecting between Acrylonitrile Butadiene Styrene (ABS) and High-Density Polyethylene (HDPE) defines long-term impact tolerance and environmental resilience:
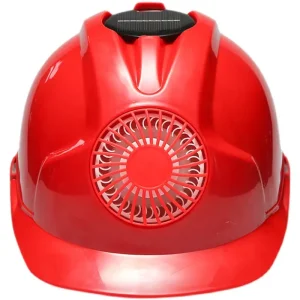
A frequent challenge with black helmets is heat absorption on exposed outdoor sites. As a premier black safety helmet manufacturer, our production integrates twin cooling strategies: aerodynamic channel venting and thermal dispersion suspension systems. By placing directional vents on the upper crown protected by interior baffles, convective currents vent warm air upward without reducing vertical impact protection or letting in falling debris.
End-to-end original equipment manufacturing, turnkey customization, and container-level procurement efficiencies.
Complete logo silk-screening, pad printing, and reflective corporate livery engineered for extreme industrial environments.
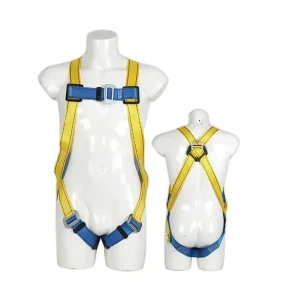
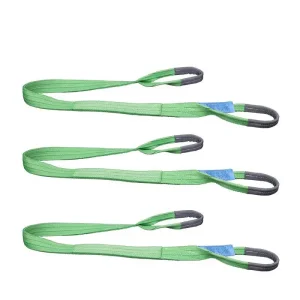
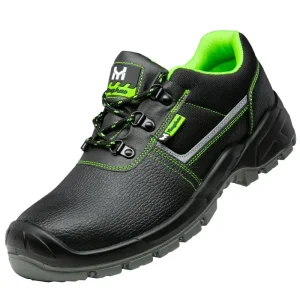
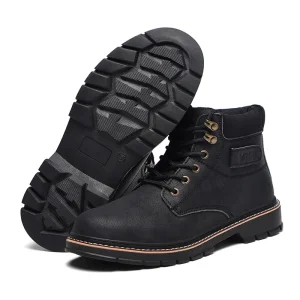
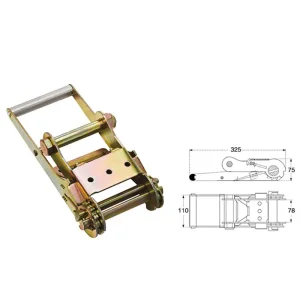
Consolidate your black safety helmet orders directly with lifting slings, ratchet tie-downs, harnesses, and safety footwear under one customs manifest.
Factory-integrated 30mm universal accessory slots designed for quick clip-on earmuffs, mesh face shields, and integrated welding visors.
Every shipment undergoes in-house batch testing for vertical shock absorption, lateral deformation resistance, and low-temperature impact tolerance.
Exceeding international regulatory benchmarks while developing intelligent head protection systems.
Our black safety helmet solutions are engineered to meet and exceed EN 397:2012+A1:2012, ANSI/ISEA Z89.1-2014 Type 1 Class C/G/E, and GB2811-2019 standards, ensuring broad market readiness and compliance acceptance.
Our upcoming engineering roadmap features smart helmet systems with integrated micro-sensors for fall detection, environmental gas monitoring, heat stress evaluation, and NFC emergency health profiling for isolated workers.
We are advancing closed-loop recycling processes to incorporate up to 30% recycled engineering polymers into inner support cradles and non-critical headgear structural parts without reducing shell impact safety ratings.
Technical and commercial clarifications for enterprise procurement professionals and regional PPE importers.
While dark surfaces absorb more radiant light energy, our industrial black safety helmets counter this by using infrared-reflective carbon pigments and ventilated shell air channels. In direct field trials, the temperature inside our ventilated ABS black shells remains within 1.5°C of standard white helmets.
Standard industry guidelines suggest replacing the shell within 3 to 5 years from first deployment, depending on environmental stress and UV exposure. Our UV-stabilized ABS formulations are designed to maintain impact attenuation thresholds for up to 5 full years under typical outdoor conditions.
Our baseline factory MOQ for custom private-label silk-screened or pad-printed black safety helmets starts at 500 units. For fully customized shell designs or proprietary tooling requirements, our engineering design team provides custom manufacturing terms based on projected volume.
Yes. We supply comprehensive factory batch test reports for each production lot. These include force transmission, penetration testing, flame resistance, and lateral rigidity data compliant with EN 397 and ANSI Z89.1 specifications.
Complete your supply container with integrated fall protection systems, industrial lifting slings, and certified protective footwear.