Procure certified industrial-grade headwear, fall arrest gear, and comprehensive protective equipment straight from specialized production lines.
In modern industrial operations, head injury prevention has shifted from rudimentary rigid plastics to complex kinetic absorption, microclimate climate-control systems, and multi-sensor IoT ecosystems.
Standard Polyethylene (PE) shells are yielding to High-Impact Acrylonitrile Butadiene Styrene (ABS) and Polycarbonate-PBT alloys. These structural resins optimize strength-to-weight performance, dispersing dynamic top impact energy exceeding 5.0 kN and side-impact (lateral deformation LD) loads without catastrophic shattering.
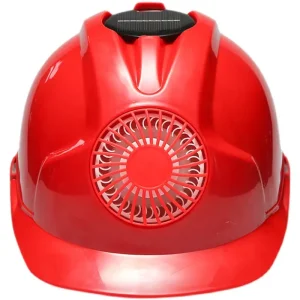
Thermal fatigue in offshore oil fields, desert infrastructure, and metal smelting creates acute safety violations when workers remove gear. Our modern industrial helmets integrate aero-dynamically engineered sliding airflow vents and built-in micro-fan convective channels that decrease intracranial heat buildup by up to 4.2°C.
Traditional hard hats protect against direct linear vertical impacts. Contemporary engineering prioritizes angular rotation dissipation. Utilizing multi-point floating suspension harnesses woven with 210D AA-grade high-tenacity fibers, shear impact forces on cerebral vasculature are reduced by over 35%.
Procurement directors in Fortune 500 engineering, EPC contracting, and logistics consortiums demand comprehensive reliability, supply chain resilience, and certified testing over pure low-bid pricing.
Multi-site EPC enterprises cannot tolerate lot-to-lot variance. Sourcing requires automated computerized injection moulding, in-line ultrasonic shell thickness testing, and lot-tracked drop-tower kinetic stress test documentation before export sign-off.
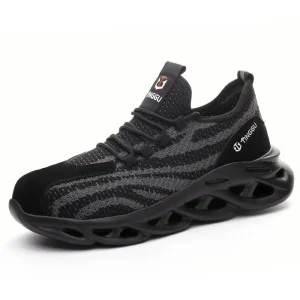
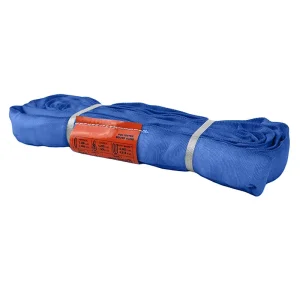
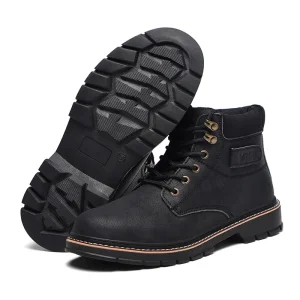
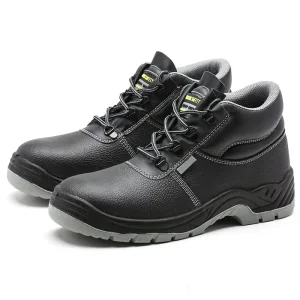
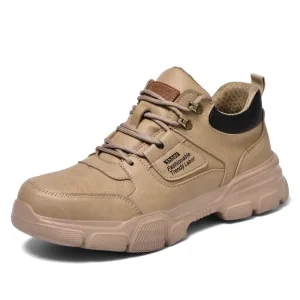
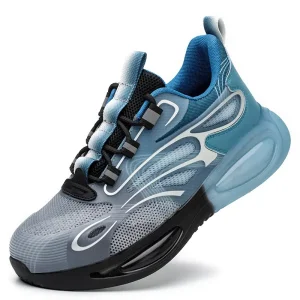
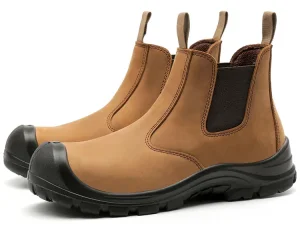
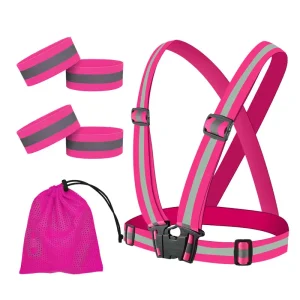
Procuring headwear in isolation inflates freight and custom-clearance overhead. Tier-1 buyers demand integrated factory manufacturing combining men safety helmets, fall-arrest full body harnesses, cargo lashing, safety footwear, and high-visibility apparel in consolidated FCL shipping containers.
Global operators need equipment dual-certified across EN 397 (Europe), ANSI/ISEA Z89.1 (North America), and GB2811 (China). Sourcing unified helmet architectures eliminates duplicate inventory across trans-continental projects.
Engineered adaptations configured to resolve unique environmental, electrical, chemical, and mechanical risks across demanding vertical markets.
Primary Hazards: Wind-shear displacement, fall-arrest impact recoil, high UV radiation degradation.
Engineering Solution: Non-vented or high-impact ABS short-brim shells equipped with a 4-point chin strap system (compliant with EN 12492 mountaineering & EN 397 industrial standards) ensuring helmet retention during high-velocity drops, combined with integrated UV-stabilizer additives.
Primary Hazards: Falling rocks, confined space impact, explosive volatile gas accumulation (ATEX), caustic chemical splashes.
Engineering Solution: Anti-static surface treated high-density polyethylene (HDPE) shells featuring built-in intrinsically safe headlamp brackets, reflective perimeter prisms, and chemical-resistant visor docking interfaces.
Primary Hazards: Arc-flash thermal release, electrical shock transfer through conductive structural components.
Engineering Solution: Dielectric Class E (ANSI) / 440V AC (EN 50365) zero-metal helmet configurations built from monolithic thermoplastic injection without ventilation holes, preventing spark ingress and electro-conductive grounding paths.
| Application Sector | Primary Material | Impact Rating | Dielectric Class | Suspension Architecture |
|---|---|---|---|---|
| Wind & High-Altitude Work | High-Impact ABS / Polycarbonate | EN 12492 / EN 397 (Front, Side, Top) | Class C / Conductive Venting | 6-Point Webbing + Ratchet Chin Strap |
| Underground Mining & Tunnelling | Reinforced HDPE Anti-Static | EN 397 Top & Lateral LD Rigid | Class G (2,200V Proofing) | Heavy-Duty Ratchet + Sweatband Cushion |
| Heavy Construction & Infrastructure | Virgin ABS Multi-Rib Core | ANSI Z89.1 Type I & II Class E | Class E (20,000V Dielectric) | Wheel-Ratchet Suspension + Goggle Slots |
| Smelting & Foundries | High-Temp Polyamide (PA66) / Fiber | EN 397 Molten Metal (MM) +150°C | Class G / Flame Retardant Shell | Aramid Heat-Resistant Suspension Core |
How Tianjin ZhongQi Growth Technology eliminates cross-border compliance friction with systematic quality control, from raw polymer verification to port-side loading.
Every production run undergoes destructive batch sampling inside our Tianjin test facilities. Using calibrated hemispherical and flat strikers dropped from automated towers, we verify force transmission remains well below the international 5.0 kN threshold under extreme moisture and thermal conditioning.
We supply international distributors with certified test reports, declarations of conformity (DoC), and user instruction manual sheets translated into English, Spanish, French, Arabic, and German. This enables smooth local customs audits without costly shipment holds.
Permanent internal calendar dial moulding guarantees traceability of polymer batch, manufacture date, and production line. We support custom corporate Pantone matching,Pad printing, reflective film heat transfers, and custom barcode packaging designed to elevate brand authority.
The convergence of active hazard sensing, ultra-light bio-polymers, and integrated telematics is shaping the next generation of head protection.
Modernized helmets are evolving into wearable edge-computing nodes. Research roadmaps feature embedded carbon monoxide (CO), hydrogen sulfide (H2S), and ambient thermal sensors that trigger acoustic and visual alerts to save workers before loss of consciousness occurs.
Tri-axial MEMS accelerometers built directly into the helmet chassis measure sudden G-force decelerations. In the event of a man-down or scaffold drop, Bluetooth Low Energy (BLE) or LoRaWAN transceivers transmit real-time GPS coordinates directly to site rescue teams.
ESG procurement initiatives are driving the switch from virgin fossil-based polyolefins to post-consumer recycled (PCR) composites and bio-sourced polymers without sacrificing impact absorption, cold fracture thresholds, or UV lifespan.
Direct technical answers to common questions raised by industrial buyers, QA managers, and safety compliance directors.
HDPE helmets typically deliver an operating service life of 2.5 to 3 years under active outdoor UV exposure. Premium virgin ABS helmets, reinforced with UV inhibitors, maintain impact deflection structural integrity for up to 5 years, provided they have not absorbed a major kinetic blow or chemical compromise.
EN 397 covers industrial safety helmets with a chin strap designed to release at 150-250 N to prevent strangulation near heavy machinery. EN 12492 (mountaineering & high-altitude working) mandates a strap strength exceeding 500 N to keep the helmet locked in place during repeated rebound falls.
Yes. Our integrated factory located in Shuangjie Trusted Industrial Park, Tianjin produces safety helmets, EN 361 fall-arrest harnesses, webbing cargo tie-downs, and industrial footwear under unified quality control, allowing buyers to consolidate mixed PPE shipments without trading house markups.
Standard production colors (white, yellow, blue, red) carry an MOQ of 500 units. Custom Pantone-matched shell injections and multi-position screen printing typically require 1,000 to 2,000 units, supported by rapid pre-production 3D samples and test reports.
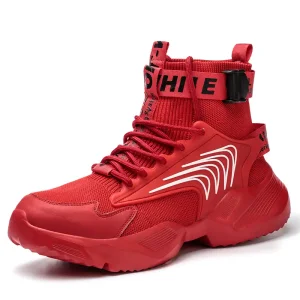
Round out your safety orders with factory-direct anti-smash footwear, lifting slings, and heavy cargo securement gear designed for peak performance.