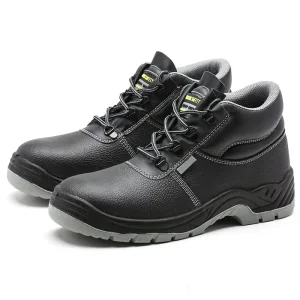
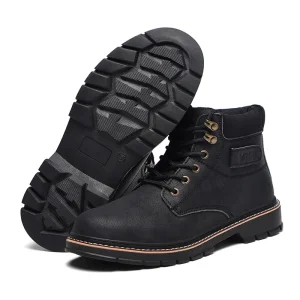
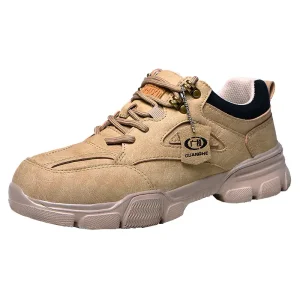
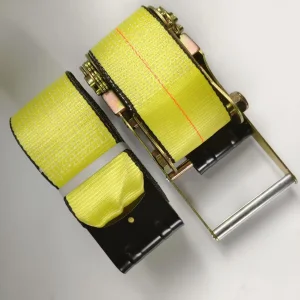
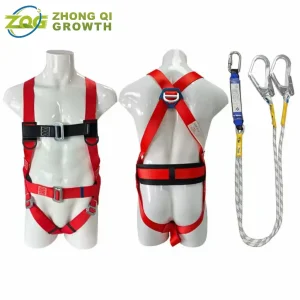
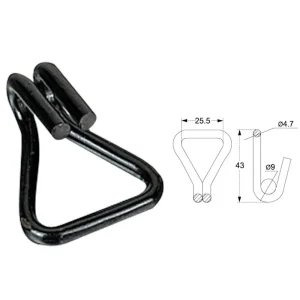
From heavy-duty ballistic head protection tooling to drop-forged rigging hardware and tactical safety footwear, our integrated production lines supply industrial-grade personal protection systems globally.
The worldwide personal protective equipment (PPE) headgear manufacturing ecosystem is undergoing an unprecedented technological transition. Navigating rigorous impact physics and automated high-cavitation tooling requires profound engineering precision.
In high-stakes industrial environments, the structural integrity of personal protective equipment begins not at the assembly bench, but within the subterranean steel cores of precision-machined injection molds. Global demand for occupational safety helmets is projected to surpass multi-billion dollar valuations, driven by intensifying occupational safety statutes across North America, the European Union, Southeast Asia, and Australasia. Procurement teams seeking to buy safety helmet molds from certified supplier and suppliers must evaluate far more than basic tooling geometry; they must audit thermal dissipation kinetics, anisotropic shrinkage compensation, multi-cavity balancing, and metallurgical endurance under relentless multi-megapascal clamping forces.
Industrial molders frequently encounter catastrophic bottlenecks when procuring lower-tier tooling: non-uniform wall cooling that yields excessive warpage, residual internal stress risers that fail dynamic EN 397 drop-tower penetrations, and micro-flashing at parting lines that demands manual deburring. A premier safety helmet mold supplier integrates advanced computer-aided engineering (CAE), German DIN-grade mold steels, high-efficiency hot runner valve gating, and conformal cooling circuits. This eliminates micro-structural flaws, maximizes resin flow uniformity for high-viscosity Acrylonitrile Butadiene Styrene (ABS) or High-Density Polyethylene (HDPE), and guarantees sub-35-second cycle times at zero-defect yield rates.
Full 3D finite-element mold-filling simulations model melt-front progressions, shear rate spikes, air entrapments, and fiber orientation, guaranteeing optimal gate location before steel cutting starts.
Direct Metal Laser Sintering (DMLS) 3D-printed tool inserts follow the exact parabolic contour of the helmet crown, eliminating hot spots and accelerating heat extraction by 28% compared to gun-drilled cooling.
Tapered alignment interlocks and self-lubricating graphite guide bushings neutralize side-thrust displacement under 650-ton injection clamp pressure, assuring zero parting line mismatch or flash formation.
Direct comparative engineering data evaluating tool steel grades, cavity layouts, cooling kinematics, and runner technologies implemented across our industrial mold platforms.
| Tooling Specification Metric | Commercial Grade Tooling | Export High-Yield System (ZhongQi Tech) | Engineering Compliance Target |
|---|---|---|---|
| Core / Cavity Steel Selection | P20 (1.2311) Pre-hardened | BÖHLER S136 / DIN 1.2083 / Assab 718H Vacuum Quenched | HRC 48–52 Uniform Core Hardness |
| Mold Base Construction | Standard C45 Carbon Steel | LKM Standard 1050 / 1.1730 Stress-Relieved Plate | Zero Deflection Under 800T Clamping |
| Runner & Gating Technology | Cold Sprue with Edge Gate | YUDO / Mold-Masters Synchro-Plate Sequential Valve Gate Hot Runner | Zero Sprue Waste, Symmetrical Pressure |
| Cooling System Kinematics | Linear Gun-Drilled Baffle Ports | Conformal 3D Spiral Circuits with Beryllium-Copper Inserts | Thermal Variance Across Shell < 2.5°C |
| Ejection & Demolding Action | Standard Mechanical Ejector Pins | Multi-Stage Hydraulic Stripper Plate + Angle Lifters for Accessory Slots | Ejection Stress Concentration < 8 MPa |
| Expected Production Tool Life | 300,000 – 500,000 Shots | 1,000,000 to 1,500,000 Guaranteed Cycles | SPI Class 101 Production Standard |
Hydraulic core-pulling slides precisely form adjustable top air vents and acoustic baffle ports without binding or flash lines.
Reinforcing structural dome ribs engineered with 0.5° to 1.5° draft angles prevent sink marks on glossy external shell surfaces.
Integrated tool inserts form standardized 30mm universal slots for earmuffs, face shields, and headlamp brackets directly in-mold.
Quick-change date stamps, safety certification engravings, and branding inserts allow rapid changeovers without dropping the mold base.
Hard-hat safety regulations require uncompromising metallurgical consistency. Our molds produce safety helmets that effortlessly satisfy mandatory international impact and electrical insulation benchmarks.
A safety helmet is a critical lifecare asset subject to intense legal scrutiny across global jurisdictions. When industrial buyers source tooling, any microscopic wall variance can lead to non-conformance during ballistic drop hammer tests or high-voltage arc tests. In Europe, EN 397:2012+A1:2012 dictates that a 5.0 kg hemispherical striker dropped from 1 meter must transmit no more than 5.0 kN of force to the test headform. In North America, ANSI/ISEA Z89.1-2014 (R2019) Type I and Type II mandates both top and lateral impact resistance, alongside Class E dielectric ratings resisting 20,000 volts without dielectric breakdown.
Our tooling design accounts directly for polymer molecular orientation during the dynamic injection phase. By deploying sequential pin-point hot gates, our molds eliminate weld lines (knit lines) in the apex and crown zones where impact loads concentrate. Furthermore, the mold wall dimensions are compensated with calibrated finite-element shrink matrices, guaranteeing that finished ABS, HDPE, or Polycarbonate/PBT shells adhere to uniform 2.2mm–3.5mm cross sections. This structural uniformity guarantees absolute compliance across CSA Z94.1 (Canada), AS/NZS 1801 (Australia/New Zealand), and GB 2811 (China) test methodologies.
Zero weld-line porosity prevents microscopic moisture paths, ensuring Class E electrical safety helmets pass 20 kV immersion breakdown tests without spark punch-through.
Internal stress-relieved mold geometry permits low-temperature resin processing, ensuring shells endure 5.0 kg striker impacts at -30°C without brittle shatter.
Crown ribbing geometry designed into the mold cavity delivers verified lateral deformation resistance under EN 397 (transverse loading up to 430 N with <40mm deflection).
From ultra-ventilated civil engineering hard hats to explosion-proof subterranean mining shells, discover specialized mold architecture suited to regional industrial workflows.
Designed for multi-cavity ABS injection. Features dynamic mold sliders to produce deep brim gutters that channel torrential rainwater away from workers' faces, integrated with high-visibility sticker tracks.
Reinforced high-impact tooling engineered for mineral-filled polyamide or high-density polymers. Direct core integration creates reinforced lamp brackets and rear cable retainers for intrinsically safe miners' caps.
Class E/G unvented shell tooling with ultra-smooth optical-mirror cavity polishing (SPI-A1 Diamond Finish) prevents dirt accumulation and avoids microscopic fissures that compromise flashover insulation.
Engineered for high-heat polymers including modified Polycarbonate (PC). Incorporates high-temperature cartridge heaters and oil-recirculation cooling channels supporting 140°C tool operation.
Climber-style short-peak safety helmet molds conforming to EN 12492 mountaineering benchmarks. Incorporates core-side mechanical undercut sliders to shape 4-point chin strap anchor lugs directly in-mold.
Companion high-precision mold suites: 16-cavity hot-runner tooling for LDPE suspension headbands, ratcheted dial adjustment pinions, and nylon webbing attachment clips.
Industrial manufacturing is shifting rapidly toward automated Industry 4.0 paradigms. Explore how our advanced tooling research incorporates sensor-embedded cavities, multi-shot molding, and bio-polymer compatibility.
Direct integration of Kistler quartz dynamic pressure and infrared melt-temperature sensors inside the mold cavity. Closed-loop feedback directly modulates the injection screw, guaranteeing zero short-shots.
Dual-shot injection molds with internal index plates. Injects an ultra-rigid ABS structural exterior shell combined seamlessly with an internal soft-touch thermoplastic elastomer (TPE) shock-absorption liner in one setup.
Engineered modular cavity inserts that mold precision structural housings for integrated heads-up displays (HUD), carbon monoxide detectors, fall sensors, and LoRaWAN mesh communication chips.
Comprehensive answers from senior tooling directors addressing mold steel metallurgy, cavitation strategy, maintenance protocols, and international shipping logistics.
Safety helmets require optical-level surface polishing and release aggressive volatile gas vapors during the rapid injection of high-impact polymers like ABS and Polycarbonate. Pre-hardened P20 steel (HRC 28-32) suffers from chemical micro-pitting, corrosion in humid climates, and accelerated abrasive wear along sharp vent lines. Vacuum-heat-treated S136 / DIN 1.2083 stainless steel delivers a hardness of HRC 50–52, exceptional acid and corrosion resistance, and maintains high-luster mirror polishing (SPI-A1) across more than 1,000,000 continuous injection shots without maintenance recalibration.
A standard industrial safety helmet presents a projected surface area of approximately 500 to 650 cm². In a dual-cavity configuration, total projected area reaches 1,000 to 1,300 cm². Factoring in the high injection pressures required for engineering-grade ABS (typically 4.0 to 5.5 kN/cm² or ~400–550 bar cavity pressure to prevent sink marks and ensure uniform wall density), the minimum recommended machine clamping force is 650 to 800 metric tons. Insufficient tonnage creates intermittent parting-line breathing, producing dangerous flash thickness along perimeter safety flanges.
In standard multi-gate setups, polymer melt streams meet midway, forming weld lines (knit lines) where cooling frontiers freeze together. These weld lines show up to a 45% reduction in impact tensile strength. Sequential valve gating utilizes pneumatic or hydraulic actuators that keep secondary gates closed until the melt front driven by the primary gate has fully washed past the runner junction. This guarantees a single continuous, unfragmented polymer matrix across the apex of the helmet, which is essential for passing dynamic striker impact tests under EN 397 and ANSI Z89.1.
Tooling development requires structured engineering milestones: 5 to 7 business days for comprehensive 3D CAD design, DFM analysis, and Moldflow simulation; 25 to 30 days for CNC roughing, vacuum heat treatment, five-axis high-speed finishing, EDM, and wire cutting; and 7 to 10 days for mold bench assembly, conformal waterline pressure testing, and initial T1 sampling. Total turnaround is 45 to 55 calendar days from signed design freeze to dispatch of CMM-verified T1 test samples, full dimensional inspection reports, and high-definition video documentation of physical factory trials.
Complete your safety procurement ecosystem with high-tenacity lifting slings, load tie-down systems, nitrile safety gloves, and puncture-resistant industrial work shoes directly from our certified manufacturing cluster.