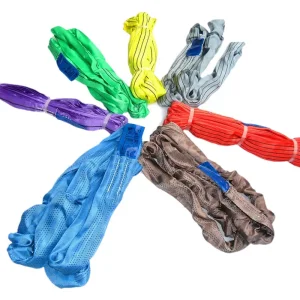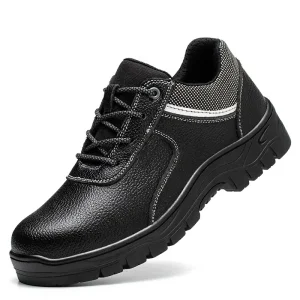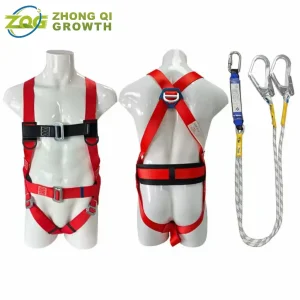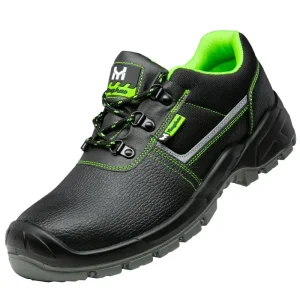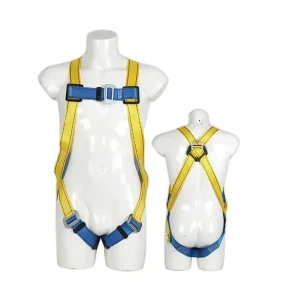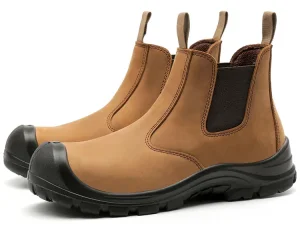
Discover high-tenacity lifting slings, rugged work footwear, and advanced load-bearing systems engineered for severe industrial duty cycles.
Analyzing the shift from commodity PPE to mission-critical, sensor-integrated head armor across Tier-1 mining groups in Australia, South Africa, South America, and North America.
Sub-surface stopes and drift galleries expose mine operators to high-velocity spalling, roof rockfall, and seismic bumps. Mining safety helmets demand Type II lateral deformation (LD) and top-crown force dispersion ratings exceeding 5.0 kN threshold tolerances under dynamic cyclic loads.
Ultra-deep mines reaching depths beyond 2,500 meters experience extreme geothermic gradient surges, relative humidity surpassing 90%, and chemical gas outgassing (methane, hydrogen sulfide). Helmet polymers must withstand constant hydrolytic degradation and high thermal creep.
Modern miners operate in complete darkness relying on intrinsically safe cordless cap-lamps, hearing defenders, active face shields, and collision-avoidance tags. Helmets require standardized universal slots (30mm Euro-slots) and mold-integrated cable retainers that eliminate catching hazards.
How Tianjin ZhongQi engineers optimize high-molecular polymers, rib-deflection spines, and 6-point suspension networks to safeguard human lives in confined worksites.
Formulated with virgin acrylonitrile butadiene styrene modified with silane coupling agents. Yields supreme surface hardness, high dielectric insulation (EN 50365 Class 0 up to 1,000V AC), and outstanding resistance against heavy falling granite fragments.
Polycarbonate blended with polybutylene terephthalate designed for smelting, blast furnaces, and hot-leach mining pits. Resists radiant molten metal splash up to 1,400°C without plastic deformation or toxic halogen fume release.
High-tenacity woven polyester harness straps cradle the skull, creating a constant 30mm deceleration standoff gap. Impact energy is redirected along the occipital ridge rather than transferring vertical compression to the cervical spine.
One-handed gloved adjustment mechanisms engineered with POM gears tested to 15,000 continuous ratcheting cycles. Ensures dynamic fit integrity even during severe head shaking, body inverted crawling, and machinery vibration.
| Performance Parameter | Standard Test Method | EN 397 Baseline | ZhongQi Mining Spec | Compliance State |
|---|---|---|---|---|
| Vertical Impact Absorption | 5kg striker drop from 1.0 meter | Transmitted Force < 5.0 kN | Transmitted Force ≤ 3.2 kN | PASS / EXCEEDS |
| Penetration Resistance | 3kg conical drop striker at 1.0m | No contact with headform | Zero perforation / no touch | PASS / EXCEEDS |
| Lateral Rigidity (LD) | Continuous transverse loading to 430N | Deformation ≤ 40mm; Residual ≤ 15mm | Deformation ≤ 24mm; Residual ≤ 6mm | PASS / EXCEEDS |
| Cryogenic Toughness | Pre-conditioning at -30°C / -40°C | Optional test (-20°C standard) | Mandatory factory lot verification (-40°C) | PASS / EXCEEDS |
| Electrical Insulation | Proof voltage testing at 1.2 kV / 5 kV | Current leakage < 1.2 mA | Class E (ANSI 20,000V) & EN 50365 | PASS / EXCEEDS |
Configuring the right shell profiles, ventilation architectures, and accessories for divergent mining topologies and geochemical environments.
Coal extraction mandates non-ventilated helmets with antistatic additive blending (surface resistivity < 10^9 ohms) to prevent electrostatic discharge (ESD) spark ignition of methane gas and suspended coal dust. Integrated cable loops securely route miner's cap-lamp battery cabling along the rear rim.
Surface mining environments in the Atacama or Pilbara subject personnel to intense ultraviolet radiation, extreme ambient heat, and horizontal blowing dust. Here, full-brim or ventilated front-swept helmets with UV-inhibited polymer blends (UV400 stabilized) and solar-powered cooling micro-fans prevent heat stroke.
Vertical shaft sinking and raise-boring expose workers to overhead falling rock slurry and mechanical rig pinch-points. Low-profile, climbing-style helmets compliant with EN 12492 and EN 397 dual-certification incorporate 4-point chin straps rated to >50daN, preventing helmet dislodgement during free falls.
From precision multi-cavity injection mold tooling to turnkey brand packaging, we convert client design blueprints into certified head protection assets.
Our in-house tooling facility houses CNC EDM machines and 1,200-ton hydraulic injection units. We engineer custom helmet outer contours, variable wall-thickness ribs, and corporate embossed markings with rapid turnaround from CAD prototype to volume test mold.
Pantone and RAL color matching across masterbatch plastics. Deploy hi-vis fluorescent lime, safety orange, cobalt blue, and pearl white with automotive-grade UV stabilizers that prevent polymer yellowing and brittleness across multi-year field service.
Multi-color pad printing processes with solvent-free, flame-cured inks guarantee that enterprise mining company logos, safety slogans, and personnel department markers will not flake or degrade when contacted by industrial oils and battery acid.
Choose between standard pin-lock headbands, dial ratchets, replaceable antibacterial sweatbands, and padded EVA neck protectors. Chin straps are available in washable nylon or antimicrobial Nomex webbing with custom break-away release thresholds.
In-mold hollow geometries accommodate active ultra-wideband (UWB) personnel positioning tags, passive UHF RFID asset tracking chips, and BLE beacons without compromising the structural integrity or dielectric ratings of the helmet crown.
Individual branded color boxes, moisture-barrier polybags, and heavy export master cartons engineered to pass ISTA 3A transit testing. Sewn-in CE tracking tags include customized serial numbers, production dates, and country-specific barcoding.
Pioneering the convergence of lightweight composite materials, edge micro-sensors, and predictive telemetry to transform passive hard hats into proactive worker life-support nodes.
Embedding micro electro-mechanical systems (MEMS) into helmet brow-bands to monitor real-time body temperature, heart rate, and ambient CO/CH4 concentrations. Data connects via Mesh-Wi-Fi to central dispatch control.
Integrating multi-walled carbon nanotubes (MWCNTs) into ABS matrices. Lowers helmet tare weight by 35% while increasing multi-directional dynamic impact dissipation by 60%, mitigating worker neck muscle strain over 12-hour shifts.
Micro-projector heads-up displays (HUD) built into the flip-down polycarbonate visor, projecting seismic floor stress heat-maps, turn-by-turn emergency egress routes, and millimeter-wave proximity warnings for automated haulage trucks.
Headquartered in Tianjin, China's premiere maritime and safety manufacturing cluster, Tianjin ZhongQi Growth Technology Co., Ltd. ensures frictionless containerized export shipping.
Located minutes away from one of Northern China’s largest automated container terminals. Eliminates inland transit delays, expediting direct weekly container departures to Rotterdam, Hamburg, Durban, Los Angeles, and Melbourne.
Optimize your shipping budgets by bundling custom mining safety helmets together with CE EN 361 fall protection harnesses, industrial polyester webbing slings, and heavy puncture-resistant safety footwear into a single 40ft HQ container.
Every batch undergoes rigorous drop impact, flame retarding, and dielectric testing in our in-house lab. Each shipment is supplied with a comprehensive 3.1 Inspection Certificate, third-party test reports, and a full warranty guarantee.
Expert insights addressing regulatory compliance, life spans, cap-lamp integrations, and factory minimum order requirements.
Contact Tianjin ZhongQi's application engineering team today for technical data sheets, certified batch test reports, and factory direct OEM quotations.
Round out your fleet procurement with our fully compatible range of heavy-duty safety footwear, full-body harnesses, lifting belts, and weather gear.