Direct factory supply of certified technical footwear, specialized trekking ergonomics, and field-grade gear developed for high-altitude Andean environments.
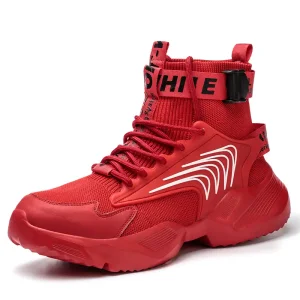
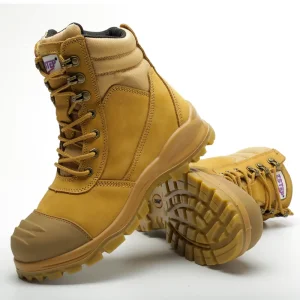
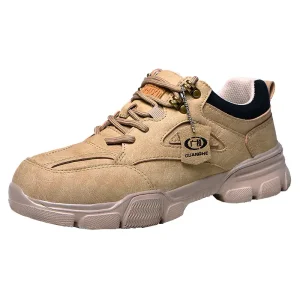
Understanding the severe tectonic biomechanics, hypobaric thermal variations, and industrial standards across Chilean copper belts and sub-polar mountain territories.
The Republic of Chile represents one of the most geographically diverse and biomechanically demanding territories in the world. Stretching over 4,300 kilometers along the Pacific rim with elevations frequently surpassing 5,000 meters above sea level across the High Andes (Cordillera de los Andes), Chilean industrial and mountaineering operations require footwear engineered far beyond generic recreational hiking standards. In critical regions such as Antofagasta, Tarapacá, and Atacama—home to premier global open-pit and underground copper, lithium, and molybdenum operations like Chuquicamata, Escondida, and Collahuasi—crews operate at extreme hypobaric altitudes where oxygen-depleted atmospheres and sharp thermal oscillations (shifting up to 35°C within a single 12-hour operational window) impose massive physical degradation on standard rubber compounds and synthetic adhesives.
In addition to extreme altitude, Chilean mountaineering and industrial field operations contend with hyper-abrasive mineral scree, basaltic volcanic soils, saline brine surfaces (Salares), and sharp copper-rich tailings. Conventional safety footwear fails prematurely in these environments through delamination of outsoles, puncture of puncture-resistant midsoles by razor-sharp igneous rock, and rapid hydrolysis of polyurethane layers driven by intense solar ultraviolet radiation (UV Index often peaking above 14+ in northern high-altitude operations). Moving southward into the Biobío, Los Lagos, Aysén, and Magallanes regions, the environmental profile transitions abruptly into wet Andean temperate rain forests, glaciated moraines, sub-zero Patagonian ice sheets, and permafrost conditions. These factors require specialized mountaineering boot manufacturing designed with chemical-resistant leather tanning, high-performance waterproof breathable membranes, and crampon-compatible rigid soles capable of dynamic sub-zero flex endurance.
Standard PVC and low-density PU dry out and crack within weeks under Andean solar irradiance. Our factory utilizes UV-stabilized aliphatic polyurethane foams and hydro-shielded cowhide to extend lifespan by over 240%.
Lithium brine extraction and acidic copper leach solutions in northern Chile dissolve conventional bonding cements. We engineer vulcanized dual-density nitrile rubber outsoles immune to saline chemical corrosion.
All footwear configurations engineered for Chilean commercial importers meet or exceed the rigorous safety parameters mandated by the National Geology and Mining Service (SERNAGEOMIN) and Norma Chilena Oficial.
A multi-layered biomechanical defense against alpine hypothermia, acute mechanical trauma, and rough scree slope fatigue.
Standard work boots transmit severe cold through the outsole into the foot bed via conductive thermal bridging. Our factory integrates sub-millimeter nanoporous Aerogel insulation layers alongside 400g to 800g/m² Thinsulate micro-fiber matrices. This multi-zone barrier arrests ground conduction freezing up to -35°C without inflating bulk, maintaining nimble foot placement during technical alpine ascents or heavy equipment operation in Andean winter freezes.
For high-angle ice fields in Chilean Patagonia and frozen alpine slopes surrounding high-altitude pipelines, standard soles fail to securely mount crampons. We mold co-injected rigid TPU (Thermoplastic Polyurethane) heel and toe welts directly into the midsole assembly, ensuring rock-solid compatibility with C2 semi-rigid strap-on and C3 fully technical step-in mountaineering crampons without compromising natural walking rocker mechanics.
Intense physical exertion at extreme altitudes generates substantial foot moisture, which in sub-zero alpine conditions causes rapid frostbite and skin maceration. Our factory applies technical PTFE and functional hydrophilic polyurethane membranes calibrated to 20,000mm hydrostatic head pressure combined with 20,000g/m²/24h breathability, preventing snow slurry penetration while venting moisture vapor continuously.
Navigating loose Andean scree and fractured copper porphyry requires immense torsional stiffness to prevent ankle rollover and lateral metatarsal collapse. We engineer 3D contoured full-length carbon composite and pre-preg fiberglass lasting boards that deliver high rigidity during front-pointing while absorbing high-impact shock across extended 14-hour operational shifts.
Combining automated robotic footwear lasting, specialized cold-weather polymer compounding, and full private-label OEM/ODM agility.
Global commercial distribution of technical mountain footwear has undergone a systemic paradigm shift. The historical reliance on boutique European alpine cobblers has proven incapable of meeting the volume, lead-time reliability, and aggressive cost structures demanded by large South American mining conglomerates, state infrastructure contractors, and commercial distribution syndicates. Headquartered near the maritime logistics hub of Tianjin Port, our modern manufacturing complex bridges the critical gap between technical alpine engineering and high-throughput industrial capacity.
Our manufacturing floor integrates state-of-the-art DESMA dual-density direct injection machinery alongside traditional, ultra-rugged Goodyear welt stitching stations. For technical mountaineering lines destined for Chilean high-altitude exploration, our automated toe-lasting robots ensure uniform tensioning around 2.4mm full-grain hydrophobic perwanger-style leathers, eliminating weak points along the lower perimeter where rock abrasion frequently sparks seam blowouts. Before batch assembly, every consignment of rubber compound undergoes strict dynamic rheometer analysis to ensure cold-flex durability: soles are subjected to continuous flexing tests in cryogenic simulation chambers at -40°C for over 100,000 cycles without showing micro-fractures.
Furthermore, we support large-scale Chilean importers, private distributors, and institutional safety procurement bodies with complete private-label OEM/ODM solutions. From customized Spanish-language tongue labeling compliant with Chilean Ministry of Health (MINSAL) decree regulations to specialized laser-etched distributor branding and custom mold tooling for regional foot morphologies, our engineers offer seamless technical translation from digital CAD prototype to full 40-foot high-cube container consignments.
Ensuring frictionless import clearance through Customs and complete legal conformity with Chilean labor safety inspection authorities.
Rigorous verification of toe-cap impact resistance (200 Joules) and puncture resistance (1100 Newtons) mandated by the Instituto de Salud Pública (ISP).
Electrical hazard testing validating insulation integrity up to 14,000 Volts at 60 Hz for mining substations and alpine high-voltage transmission lines.
Conformity with high-altitude open-pit and underground safety directives (DS 132 Mining Safety Regulations) across Tarapacá and Antofagasta.
Full support for preferential tariff treatment under the Free Trade Agreement, securing 0% customs duty entry into Valparaíso and San Antonio.
Engineered for mission-critical deployments across distinct geographical zones of the Chilean industrial ecosystem.
De-icing crews, surveyors, and geological drilling personnel operating in Calama, Chuquicamata, and high Atacama basins require extreme insulation against frozen mineral mud and dry, sub-zero winds. Footwear configurations in this theater emphasize 600g thermal linings, non-metallic composite safety toe caps (eliminating cold conduction inherent in steel caps), and high-traction self-cleaning outsoles.
Andean water diversion corridors, penstocks, and wind turbine installations located along the mountainous passes of Maule, Biobío, and Araucanía subject technicians to damp scree and wet rock. Our hybrid alpine boots feature breathable waterproof bootie construction, dual-density PU midsoles for sustained energy return, and rigid heel counters to stabilize step-climbing on steep grade embankments.
Scientific research and eco-expeditions traversing the Southern Patagonian Ice Field (Campos de Hielo Sur) demand technical crampon compatibility and 100% impervious water protection against glacial slush. We supply double-boot modular configurations featuring removable insulated thermo-formable booties encased within an ultra-abrasion Kevlar-reinforced outer gaiter shell.
Tactical rescue personnel operating in emergency alpine terrain require rapid lacing systems (such as high-tensile steel BOA-type dials), enhanced lateral ankle stability cuffs, and high-visibility retro-reflective inserts. Footwear designed for these first-response units balances ultra-light structural weight with ballistic rubber perimeter randing.
Driving forward the next decade of alpine protective technology through advanced materials science and biomechanical ergonomics.
Integrating graphene nanoplatelets into vulcanized nitrile rubber compounds to increase wet-ice grip by 45% while decreasing outsole weight by 22% compared to standard carbon-black rubber.
Prototyping low-energy sub-zero IoT telemetry chips embedded in the heel arch to monitor real-time worker fatigue, ambient temperature drops, and sudden slips across remote Andean operations.
Transitioning to plant-based non-petroleum PU midsoles and fluorine-free dynamic water-repellent (DWR) surface finishes, aligning with strict environmental mandates in Patagonia.
Harnessing generative AI anatomical scanning databases of South American male and female foot profiles to manufacture custom orthopedic lasting shapes directly at industrial volume.
Essential guidance on importing, customizing, and specifying technical mountaineering boots from our manufacturing facility.
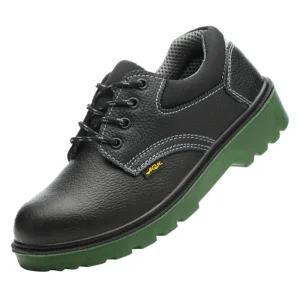
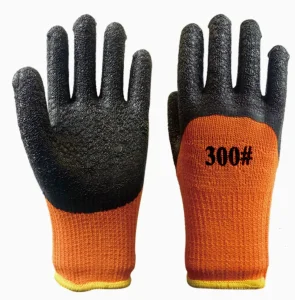
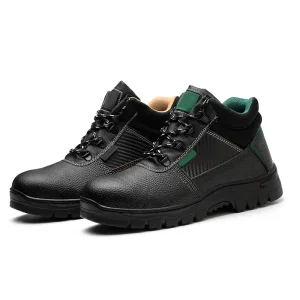
Factory-direct industrial mountaineering boots, specialized mountain gloves, protective footwear, and high-tensile rigging solutions engineered for demanding Chilean worksites.
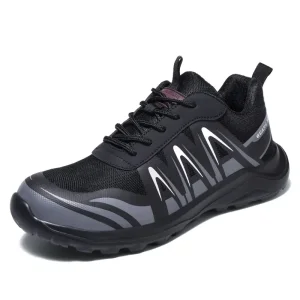
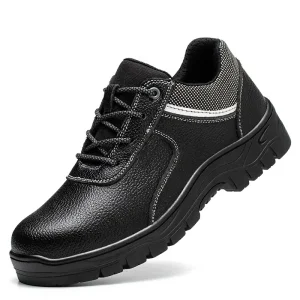
Plan your customized OEM/ODM production run, request official test reports (CE EN ISO 20345 / NCh 772), or obtain factory direct FCL pricing with China-Chile FTA Form F tariff-free documentation.
